High-efficiency polymer melt filter cartridges, leaf disc filters, and plastic pelletizing equipment engineered for ultra-low pressure drop and high purity throughput.
In modern polymer processing and plastic recycling industries, selecting premier plastic pelletizing machine manufacturers & companies directly dictates thermal stability, melt homogeneity, and the physical characteristics of recycled resin pellets. As global environmental mandates like the EU Single-Use Plastics Directive and US recycled-content thresholds tighten, resin producers and plastic recyclers require advanced granulating machinery that balances intense thermal mechanical stresses with strict energy conservation standards.
Pujiang HG Plastic Machinery Co., Ltd. leads this industrial transition. Over two decades, our plant has merged precision twin-screw melt homogenization, intelligent multi-channel continuous screen changing, and sub-micron polymer filtration into single turnkey pelletizing production lines. Whether processing post-consumer recycled (PCR) polyolefins (PP/PE), post-industrial waste (PIR) film scrap, or engineering plastics (PET, PA, ABS, PC), high-capacity pelletizing demands zero thermal degradation, continuous degassing, and strict melt viscosity maintenance.
Selecting the optimal cutting technology depends on melt flow index (MFI), polymer viscosity, moisture percentage, and desired pellet geometry.
Designed specifically for non-hygroscopic polyolefins (HDPE, LDPE, LLDPE, PP) and lightly filled compounds. The polymer melt is cut immediately at the die plate surface, cooled by a high-velocity rotating water ring inside the cutting chamber, and centrifugal drying conveys solid spherical pellets.
The industry gold-standard for high-capacity compounding, micro-pellet creation, and moisture-sensitive or low-viscosity elastomers (TPE, TPU, EVA, Hot Melt Adhesives, Bio-polymers). The die face operates submerged under pressurized hot water, preventing die-hole freezing and ensuring uniform spherical geometry.
Ideal for high-tensile engineering polymers (PA6, PA66, PBT, PET, PC) and glass-fiber reinforced composites (up to 50% GF content). Continuous extruded molten strands pass through a cooling bath before entering high-speed rotary helical blade cutters for precise cylindrical pellets.
Engineered for water-sensitive materials such as PVC compounds, starch-based bioplastics, and high-filler calcium carbonate masterbatches. High-efficiency centrifugal blowers quickly freeze cut pellets in a dry vortex, avoiding hydro-degradation.
| Pelletizing Technology | Compatible Polymers | Throughput Range | Pellet Shape & Uniformity | Cooling Mechanism |
|---|---|---|---|---|
| Water-Ring Die-Face | PE, PP, PS, EVA, Low-fill Composites | 150 kg/h – 2,500 kg/h | Lenticular / Disk spherical (Very Good) | Circulating Water Ring + Centrifugal Dryer |
| Underwater (UWP) | TPU, TPE, PET, PLA, MFI > 30 Polyolefins | 300 kg/h – 8,000 kg/h | Micro / Micro-spherical (Exceptional) | Submerged Pressurized Water Loop |
| Strand Cutting | PA66, PBT, ABS, PC, Glass Fiber Compounds | 100 kg/h – 4,000 kg/h | Cylindrical / Regular (Good) | Water Trough + Air Knife De-watering |
| Air-Cooled Cutting | Rigid/Flexible PVC, PLA Starch Blends | 100 kg/h – 1,200 kg/h | Spherical / Irregular (Standard) | Dry Air Vortex + Cyclonic Air Conveying |
The quality of recycled plastic pellets and compound resin depends entirely on removing unmelted gels, metal debris, paper fibers, aluminum foil scrap, and degradation particles before melt enters the cutter. Integrating advanced polymer candle filters, leaf disc filters, and continuous non-stop screen changers ensures zero pressure spikes and stable extrusion rate.
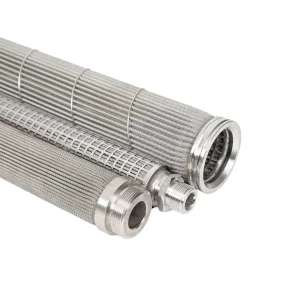
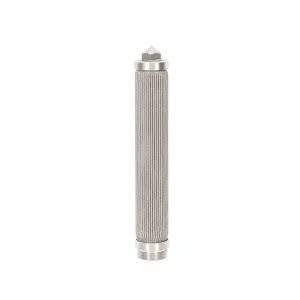
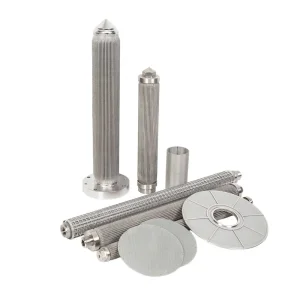
Fabricated from multi-layer SUS 316L woven wire mesh or sintered metal felt, candle filter cartridges deliver ultra-high surface filtration area within compact pressure vessels. Designed to withstand pressures up to 320 bar and temperatures exceeding 350°C, these cartridges offer micron ratings down to 5 microns.
Used extensively in high-purity PET recycling, BOPP/BOPET film recovery, and chemical fiber spinning lines. Leaf discs feature computer-modeled flow channels that prevent melt stagnation and thermal degradation, increasing filter area up to 8x compared to standard flat screen packs.
Automatic hydraulic piston screen changers enable 24/7 continuous operation. When differential melt pressure rises due to impurity buildup, automated hydraulic valves divert a small fraction of purified melt backwards to flush out contaminants without interrupting production or dropping melt pressure.
As the global polymer recycling industry shifts toward digital manufacturing and circular closed-loop systems, pelletizing hardware must evolve across four key technical fronts.
Real-time online viscometers will continuously measure melt viscosity (MFI) right before the die plate. AI algorithms will dynamically adjust screw RPM, barrel temperature profiles, and vacuum degassing levels to stabilize pellet MFI despite fluctuations in post-consumer feedstock quality.
Next-generation pelletizing extruders utilize electromagnetic induction heating combined with high-torque, direct-drive PMSM motors. By capturing exhaust heat from cooling water loops to pre-dry raw flakes, total specific power consumption drops from 0.35 kWh/kg to under 0.21 kWh/kg.
Meeting FDA NOL (No Objection Letter) and EFSA standards for rPET and rHDPE food-packaging requires filtration levels under 25 microns without causing thermal degradation. Advanced 3D sintered metal fiber candle filters will replace conventional wire mesh screen packs.
Current backflush screen changers waste 1–3% of polymer melt during purge cycles. Future continuous ultra-sonic pulse backwash technology will reduce purge waste to under 0.2%, maximizing resin yield and decreasing operating cost.
Pujiang HG Plastic Machinery designs customized extrusion, filtration, and pelletizing lines targeted at specific industrial supply chain challenges.
Challenge: Highly contaminated, low-bulk-density agricultural film and stretch film (LDPE/LLDPE) containing sand, paper, and moisture up to 10%.
HG Solution: Integrated cutter-compactor shredding system combined with double-stage (cascade) twin-screw venting extruders. Equipped with dual triple-vacuum degassing zones and high-capacity dual-piston continuous backflush screen changers, delivering clear, bubble-free PE pellets for blown film reuse.
Challenge: Processing milk bottles, detergent containers, and caps containing mixed viscosity resins and residual label contaminants.
HG Solution: Single-screw high-torque extruders integrated with multi-layer sintered disc filter packs (80–120 mesh) and automatic water-ring pelletizing. Provides consistent pellet melt flow index suitable for blow molding and injection molding applications.
Challenge: Extreme sensitivity to shear heat and moisture hydrolytic degradation in polylactic acid (PLA) and PBAT bioplastics.
HG Solution: Low-shear co-rotating twin-screw extruder design with precise split barrel temperature control zones (±0.5°C). Integrated with underwater pelletizing to guarantee low thermal residence time and crystal-clear pellet appearance.
Challenge: Homogeneous dispersion of up to 80% inorganic fillers without machine barrel wear or blade dulling.
HG Solution: Bimetallic alloy barrel liners with high-chrome tungsten carbide cutter blades, paired with high-efficiency strand or water-ring pelletizers for high-density filler masterbatches.
Why leading multinational polymer enterprises partner with Pujiang HG Plastic Machinery Co., Ltd. for turnkey granulating machinery and filtration infrastructure.
From raw stainless steel bar stock machining and vacuum heat-treatment to CNC laser drilling of filter screen plates and automated dynamic balance testing of cutter heads—our 100% in-house manufacturing eliminates component sub-supplier delays.
Located in Zhejiang’s advanced manufacturing belt, HG leverages immediate access to high-grade SUS316L, Hastelloy alloys, and specialized tool steels, allowing us to deliver custom-engineered equipment 40% faster than European counterparts.
Every melt filter element, continuous screen changer, and pelletizing cutter undergoes 100% hydrostatic pressure testing, ultrasonic weld flaw detection, and coordinate measuring machine (CMM) dimensional verification before export dispatch.
Our modular design philosophy allows global plastic processors to acquire Tier-1 European standard mechanical stability and filtration precision at 30% to 50% lower total capital investment (CAPEX), delivering fast ROI.
Engineering procurement managers and plant directors must evaluate six core engineering metrics when selecting a plastic pelletizing equipment manufacturer.
Calculate total electric power (kWh) consumed per metric ton of acceptable pellets. HG machines achieve SEC values under 0.22 kWh/kg on PE/PP film recycling lines through optimized L/D screw ratios (32:1 to 40:1) and high-efficiency direct-drive gearboxes.
Extrusion pressure fluctuations at the die head must remain within ±2 bar to ensure uniform pellet mass. HG’s automatic continuous backwash screen changers eliminate pressure drops during filter screen indexing.
Excessive thermal exposure destroys polymer molecular weight. HG twin-venting vacuum chambers remove low-molecular volatiles, moisture, and printing ink odors without over-shearing sensitive polymer chains.
Processing abrasive materials like glass-filled engineering plastics or calcium carbonate masterbatch requires bimetallic barrels (matrix nickel-based alloy with 40% WC) to extend screw working life beyond 25,000 operational hours.
Ensuring seamless international installation, regulatory compliance, and rapid spare parts distribution across North America, Europe, Southeast Asia, and the Middle East.
All electrical control cabinets utilize Siemens S7-1500 PLC systems, Schneider contactors, and ABB VFD drives, fully certified under EU CE Directive 2006/42/EC and UL 508A industrial control panel standards for North America.
High-pressure melt filter housings and candle filter pressure vessels comply with EU Pressure Equipment Directive (PED 2014/68/EU) and ASME Section VIII standards, accompanied by full material traceability (EN 10204 3.1 certificates).
Equipped with secure IoT remote gateway modules, HG engineers perform real-time diagnostic troubleshooting, PLC firmware updates, and process optimization remotely. On-site commissioning engineers are dispatched within 48 hours.
Standard filter elements, screen mesh packs, seals, pelletizer blades, and die plates are maintained in strategic regional hub warehouses for 24-to-48-hour emergency dispatch, minimizing unplanned factory downtime.
Technical answers to critical questions regarding plastic pelletizing machine selection, polymer melt filter maintenance, and commissioning.
Explore our complete range of high-viscosity melt filter elements, stainless steel screen meshes, and plastic granulating recycling equipment.